Description
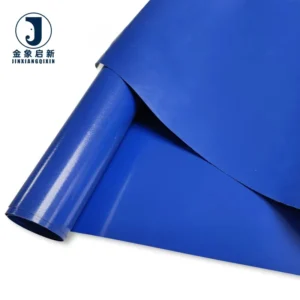
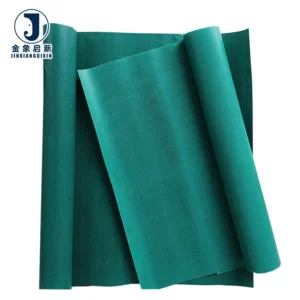
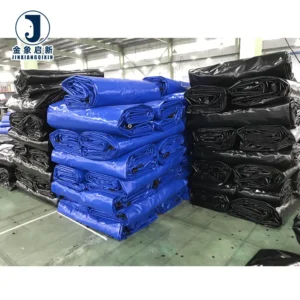
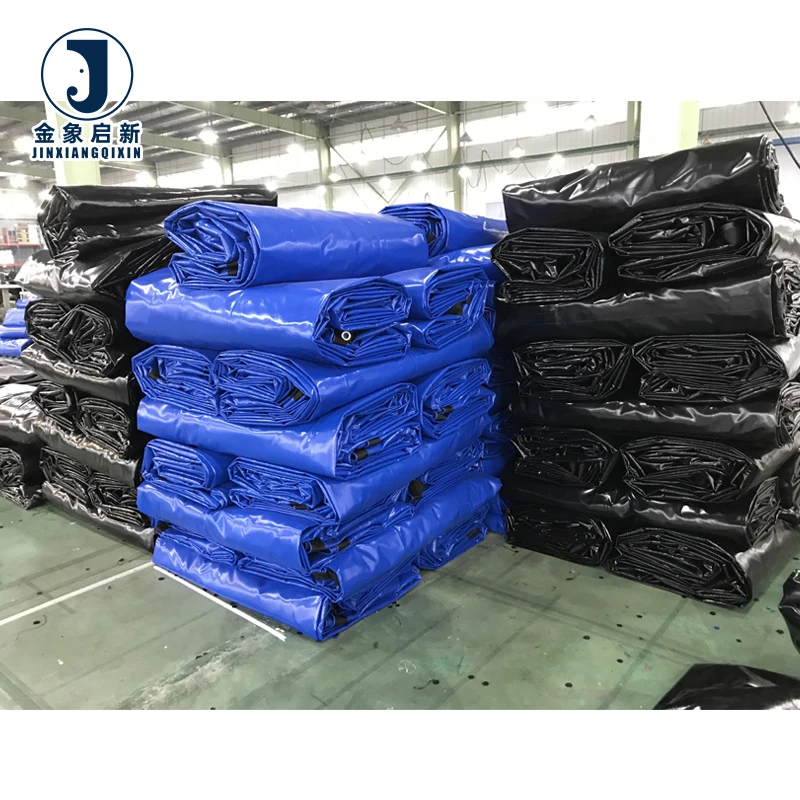
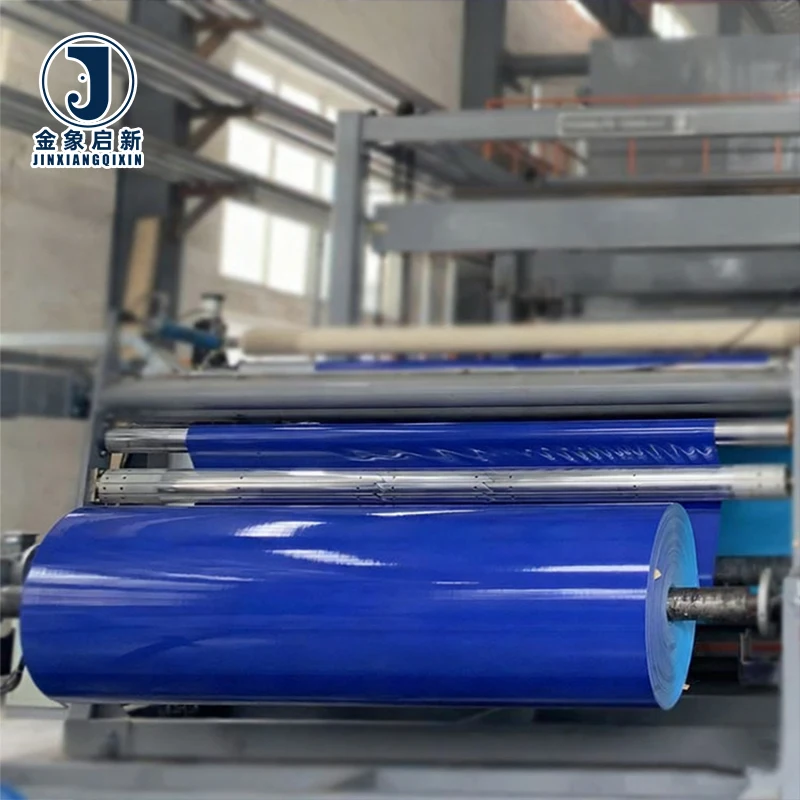
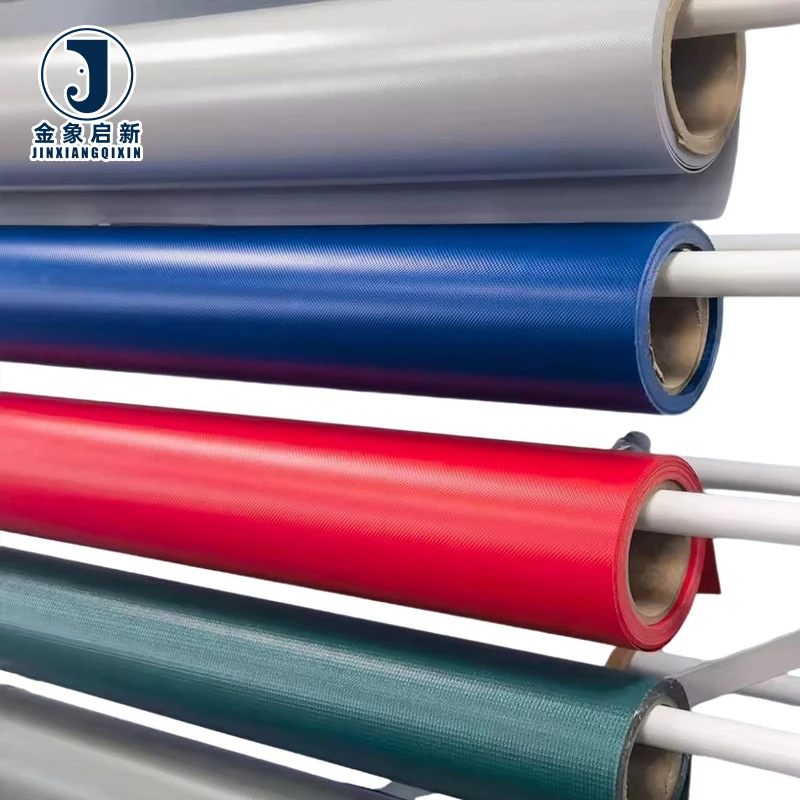
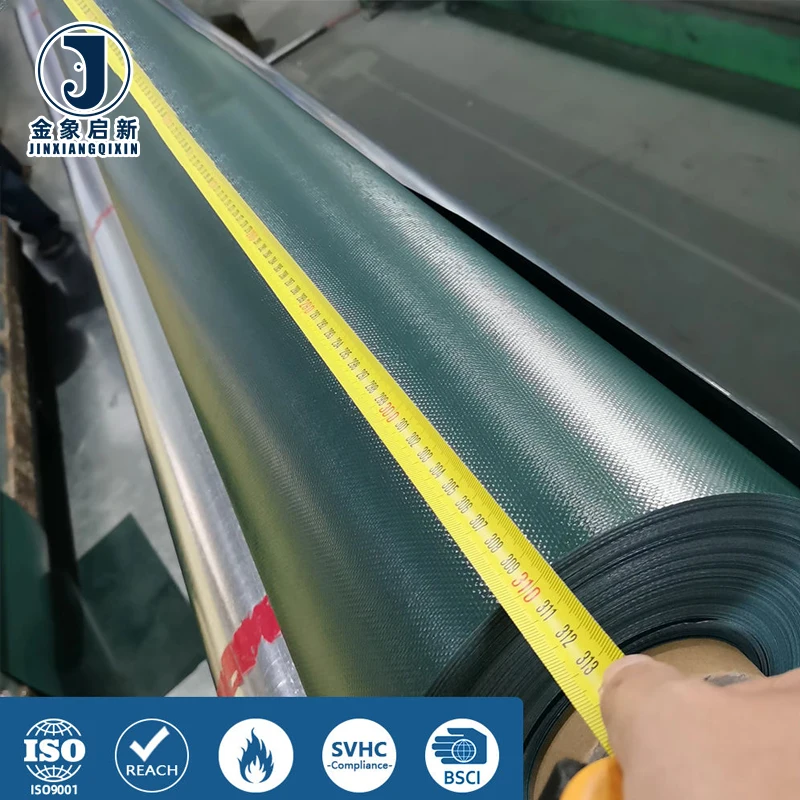
Bulk Roll Consistency — Every 650 GSM roll is weighed and colour-checked before container loading, so distributors receive matched batches ready for regional resale.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | PVC Tarpaulin Roll |
| Weight | 650 GSM |
| Coating Material | PVC (Polyvinyl Chloride) |
| Base Fabric | Polyester |
| Waterproof | Yes — fully coated construction |
| Flame Retardant | Available in flame retardant grades — confirm the grade required for your market |
| UV Treatment | UV stabilised — test basis to be confirmed per order |
| Anti-Mildew | Yes — antibacterial and mildew proof formulation |
| Welding Options | HF welding, Hot Air welding, Sewing |
| Temperature Resistance | High temperature and cold resistance — confirm operating range for your climate |
| Roll Format | Supplied in roll stock |
| Certification Framework | ISO, CE |
Application Suitability
| Application | Exposure & Requirement |
|---|---|
| Tent and awning fabrication | Repeated assembly and teardown, seam stress at ridge and wall panels, prolonged sun exposure during event seasons |
| Tensile and membrane structures | Permanent tension loading, wind-induced oscillation, structural welds carrying design loads |
| Portable storage structures | Forklift contact at base, internal condensation risk, abrasion from stored goods |
| Airport hangars and shade systems | High wind uplift, fuel and hydraulic fluid splash, wide unsupported spans |
| Stadium architectural roofs | Long-term UV exposure, thermal cycling, drainage ponding at low-slope zones |
| Outdoor industrial covers | Direct rainfall, dust and particulate ingress, mechanical damage from handling |
Why a Quoted GSM Figure Does Not Guarantee the Roll You Receive
The weight printed on the invoice is only meaningful if it is verified on the physical roll before it leaves the factory.
Buyers of PVC Coated Tarpaulin Roll wholesale stock regularly face a quiet substitution: the material arrives lighter than specified, and the shortfall only becomes apparent when the fabric is cut and fabricated into finished products. A variance of even a small percentage across a full container translates into thinner coating, reduced tear resistance, and welds that fail under load. Roll-to-roll colour drift within the same shipment compounds the problem — panels joined side by side on a tensile structure show visible banding once installed under sunlight [NEED_CITE: ISO 1421 tensile and tear test methods for coated fabrics]. The consequence is not a single defective panel but an entire production run that the end client refuses to accept.
Roll Weight Verification at Every Production Stage
Every PVC Coated Tarpaulin Roll wholesale order at this weight grade goes through dedicated QA/QC at each stage of coating, curing, and winding. The 650 GSM figure is not a nominal target — it is the measured value recorded per roll against the material specification sheet. Rolls that fall outside the tolerance band are pulled from the batch before packing. This discipline matters most for distributors who resell to fabricators: a single underweight roll in a mixed shipment damages trust far beyond its own value.
Batch Colour Matching Across Multi-Roll Shipments
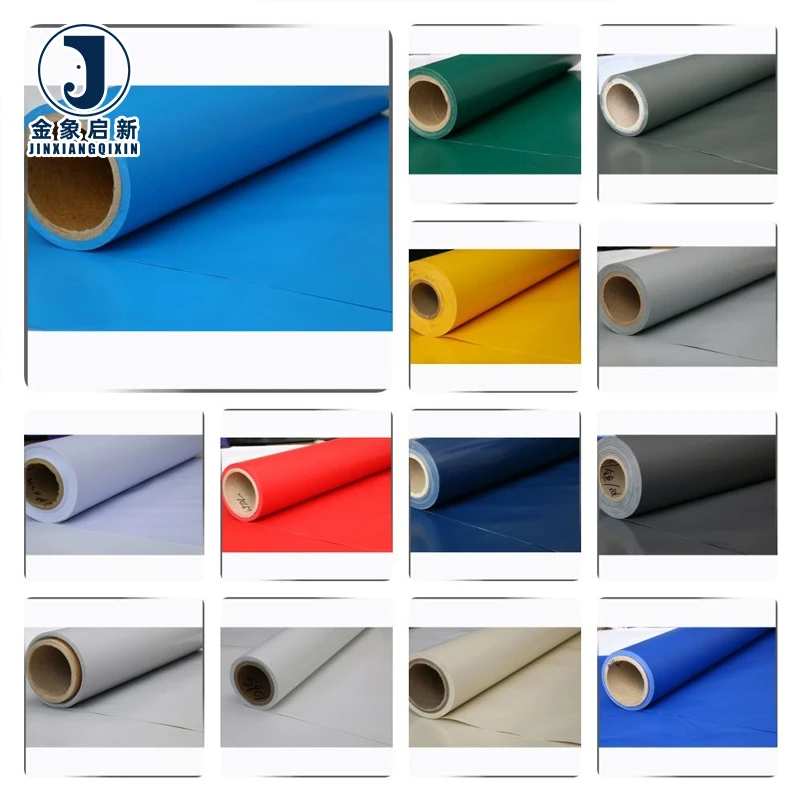
Colour consistency is controlled at the compounding stage, where pigment ratios are locked before coating begins. When a PVC Coated Tarpaulin Roll wholesale order spans several production batches, each roll is cross-referenced against the order’s colour reference card under standardised lighting. Rolls that show perceptible drift are held back. For tent manufacturers joining panels across a large canopy, this step prevents the visible seam banding that forces costly on-site replacement.
Welding Compatibility for Downstream Fabrication
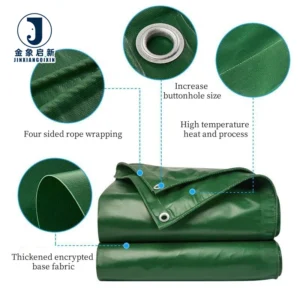
The 650 GSM construction supports HF welding, hot air welding, and traditional sewing. This range matters because fabricators serving tensile structures often specify HF welded seams for their peel strength, while tent makers may prefer hot air for curved panels and sewing for reinforced edge hems. The PVC coating formulation is engineered to melt and bond consistently across all three methods, giving fabricators flexibility without requiring separate material grades for different joint types.
How GSM and Base Fabric Interact to Define Real Performance
The 650 GSM weight is the combined mass of the polyester base fabric and the PVC coating applied to both faces. A heavier coating improves waterproofing and abrasion resistance but adds stiffness that complicates folding and packing of portable structures. The base fabric’s denier and weave density determine how well the material resists tear propagation once a puncture initiates. Coating adhesion — the bond between PVC and polyester — governs whether a welded seam holds or delaminates under tension. A roll that reads 650 GSM on the scale but uses a lighter base with thicker coating may pass the weight check yet tear more easily than a balanced construction [NEED_CITE: coating adhesion and peel strength testing for PVC-coated polyester]. Understanding this relationship helps buyers specify beyond a single number and ask for the base fabric details that match their application.
The Hidden Cost of Accepting Unverified Roll Stock
A distributor who skips pre-shipment weight verification absorbs risk silently until a fabricator reports seam failure on a tensile structure project. Investigation reveals the coating layer was thinner than specified, leaving insufficient material for a reliable HF weld. The fabricator demands replacement rolls, the distributor faces air freight charges to meet the project deadline, and the end client questions the supply chain’s competence. Similarly, flame retardant grades claimed without a supporting test report can result in a structure failing the local fire marshal’s inspection, forcing removal and reinstallation at the contractor’s expense [NEED_CITE: fire classification standards for temporary and semi-permanent membrane structures]. These are not manufacturing defects — they are verification failures that a disciplined pre-shipment process eliminates.
Why Buyers Source This Grade Here
Three full production lines and 36 sets of professional equipment provide the capacity to fill container orders without sacrificing coating consistency across rolls. The 10-person R&D team develops samples within days when a buyer requests a specific width, colour, or surface treatment, reducing the wait that typically accompanies custom PVC Coated Tarpaulin Roll wholesale orders. Dedicated QA/QC personnel inspect every roll at coating, curing, winding, and packing stages rather than relying on spot checks. Nearly 30 years of focused coated-fabric production have refined the process controls that keep GSM on target and colour uniform batch after batch. Sample development, specification matching, and documentation preparation happen under one roof, eliminating the coordination gaps that delay multi-supplier orders.
Documentation & Verification
- Material specification sheet stating 650 GSM, base fabric denier, and PVC coating weight per roll batch
- Pre-shipment inspection record with individual roll weight verification against the stated GSM
- Roll packing list detailing roll count, net weight, and container loading plan by position
- UV and flame retardant test reports supplied where applicable to the grade ordered
- ISO and CE certificates covering the production facility and quality management system
- Certificate of origin and customs documentation prepared per destination country requirements
Fabrication, Handling & Storage
- HF welding at 650 GSM requires adjusted dwell time versus lighter grades to achieve full coating fusion
- Hot air weld temperature must match PVC formulation to avoid surface scorch on this weight class
- Store rolls vertically on pallets to prevent flat-spot deformation of the polyester base fabric
- Allow cold-stored rolls to acclimatise before unrolling to avoid coating micro-cracking at low temperature
- Use mild detergent without solvents when cleaning the antibacterial mildew-proof surface
- Plan cutting layout to maximise yield from roll width, minimising offcuts on tensile structure panels
What to Include in Your Enquiry
Specify the intended application — whether tent fabrication, tensile structure, or portable storage — along with the exposure conditions the finished product will face. Confirm the fire classification or building code requirement for your target market so the correct flame retardant grade can be matched. State the roll widths and lengths that suit your production equipment, and indicate your expected annual volume so bulk pricing tiers and container loading plans can be prepared. If colour matching to an existing product line is needed, provide a physical sample or Pantone reference for the lab to work against.
Frequently Asked Questions
Q: How is GSM verified on each roll before dispatch?
A: Each 650 GSM roll is individually weighed and the result recorded on the pre-shipment inspection record. Rolls that deviate from the specification are removed from the batch before packing. The weight verification document accompanies the shipment so you can cross-check on arrival against the quoted specification.
Q: How do you control colour consistency across rolls in the same order?
A: Pigment ratios are locked at the compounding stage before coating begins. Every roll is then compared against the order’s colour reference under standardised lighting. Rolls showing perceptible drift are held back, ensuring panels cut from different rolls match when installed side by side on large-format structures.
Q: What roll widths and lengths are available, and how does bulk pricing work?
A: Multiple roll widths and lengths are available to suit different fabricator cutting tables and container loading configurations. Pricing is structured in volume tiers based on total order weight. Submit your target roll dimensions and annual volume so a tiered quotation and container loading plan can be prepared for your review.
Q: How many rolls fit in a container, and how are they packed?
A: Container loading depends on the roll width, length, and core diameter selected. Rolls are packed vertically or horizontally on pallets with protective wrapping to prevent transit damage. A detailed packing list is provided before loading, showing roll count, net weight, and position within the container for efficient unloading.
Q: What is the lead time and minimum order for custom width or colour?
A: Custom widths and colours carry specific minimum quantities and lead times that depend on the pigment and base fabric combination requested. The 10-person R&D team produces samples within days for approval before bulk production begins. Share your requirements to receive a confirmed lead time and minimum order quantity.