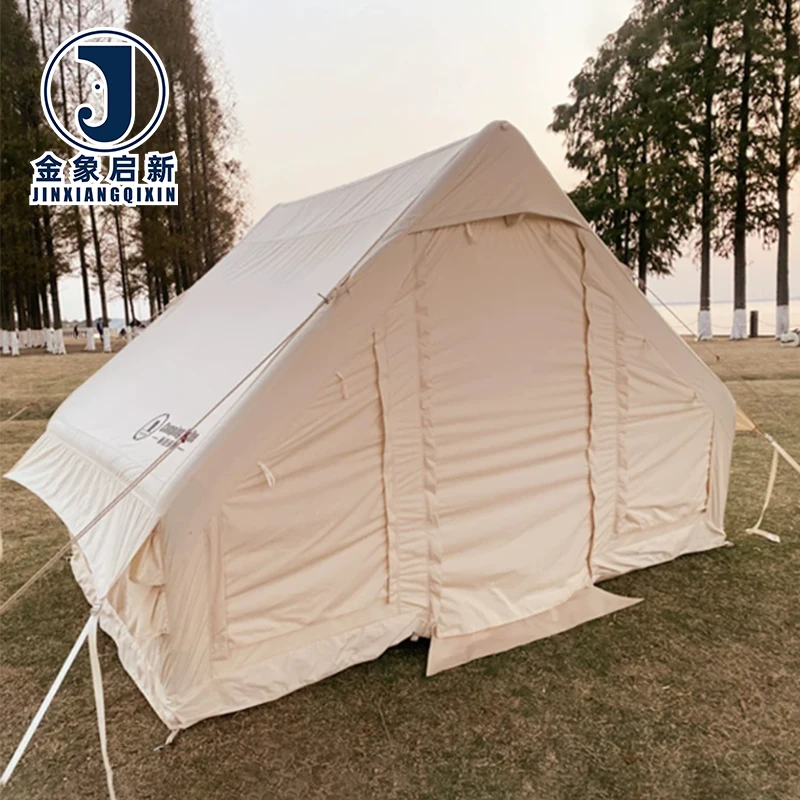
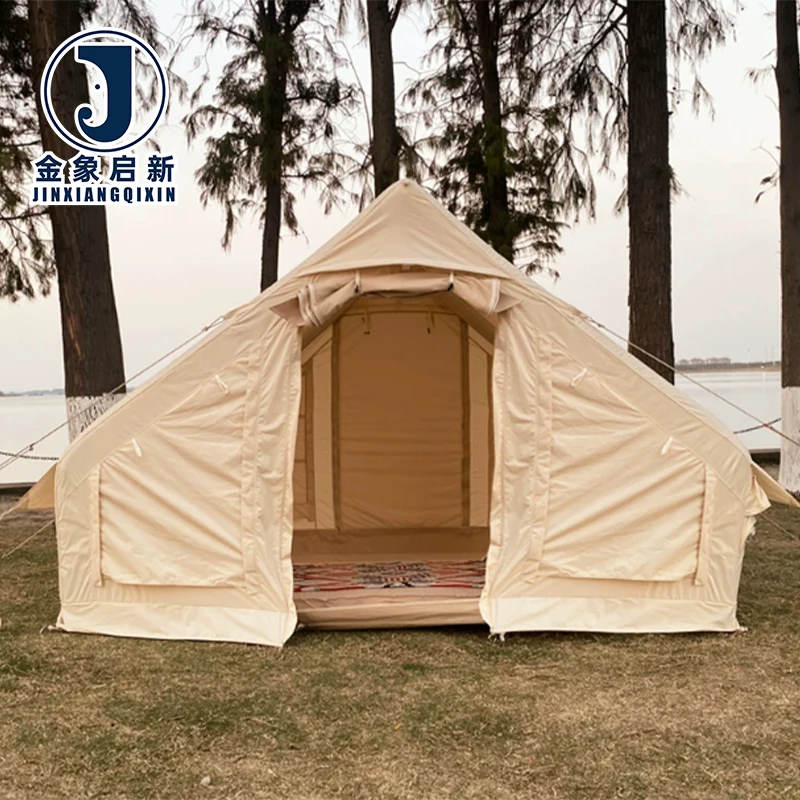
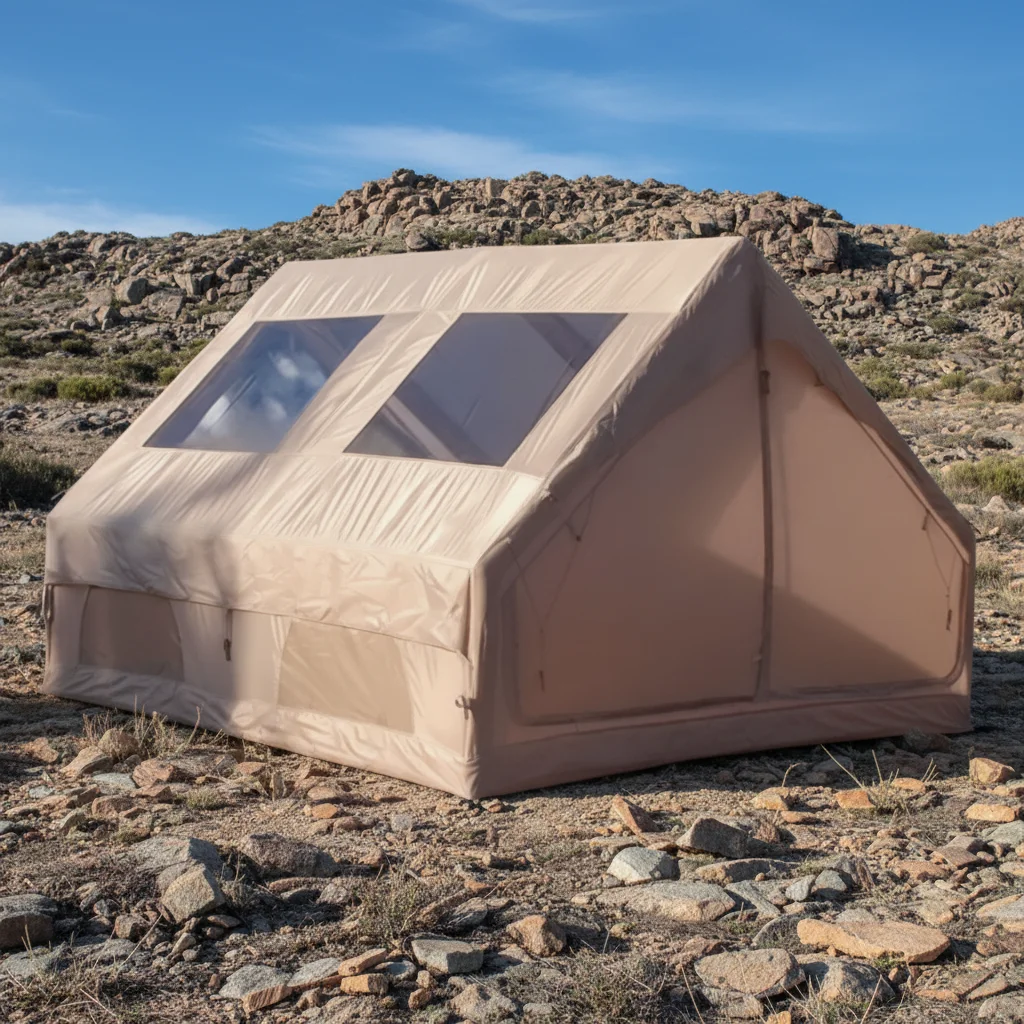
Description
Volume Consistency Across Batches — Every roll of PVC inflatable tent fabric is produced on one of three dedicated lines with in-process coating weight checks, ensuring your container load arrives with uniform GSM and colour from first roll to last.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Inflatable Tent Fabric |
| Core Material | PVC coated tarpaulin |
| Product Forms | Roll stock for 2–8 person capacity structures, single layer construction |
| Waterproof Performance | Fully waterproof coated construction |
| UV Resistance | UV-resistant treatment available (test basis not stated in source) |
| Season Rating | 4-season suitable |
| Deployment System | Quick automatic opening compatible |
| Customization Service | OEM & ODM, sample customization, pattern printing |
| Production Facility Area | 9,180 m² |
| Production Lines | 3 full production lines |
| Processing Equipment | 36 sets of professional processing equipment |
| R&D Team Scale | 10 technicians |
| Quality Control System | Full-process quality inspection with dedicated QA & QC staff |
| Certifications | ISO 9001, ISO 14001, ISO 45001, CE |
Application Suitability
| Application | Exposure & Requirement |
|---|---|
| Inflatable tent and awning manufacturers | Repeated inflation cycles, airtight seam integrity, roll-to-roll colour consistency across production runs |
| Membrane structure fabricators | Large uninterrupted surface areas, uniform coating adhesion, UV and weather exposure over extended deployment |
| Industrial shelter contractors | Temporary deployable structures, rapid setup and teardown, resistance to wind load and abrasion at anchor points |
| Mobile field operations and emergency response | All-weather protection, quick automatic opening, reliable performance across temperature fluctuations |
| Commercial outdoor event infrastructure | High-visibility branding via pattern printing, repeat-use durability, consistent appearance across multiple units |
Why Roll-to-Roll Colour Variation Sabotages Inflatable Tent Production
Batch colour uniformity starts at the coating head, not at the packing table.
When an inflatable tent manufacturer cuts panels from six different rolls and assembles them side by side, even a slight shade shift becomes visible under daylight. Buyers who have received container loads of PVC inflatable tent fabric roll stock only to find two or three noticeably different tones know the cost of re-sorting, re-cutting, and delaying shipment [NEED_CITE: colour measurement tolerances for coated fabrics per ISO 105-J02]. The frustration compounds when the order was placed as a single batch with a single colour reference. Controlling this variable requires discipline at every stage from pigment batching through coating and winding.
Coating Weight Control for Airtight Inflatable Structures
Inflatable tents demand fabric that holds internal air pressure without bleeding through the coating layer. The PVC coating must bond to the base fabric with sufficient adhesion to resist delamination when the structure flexes under wind load. Our 10-person R&D team develops coating formulations matched to the inflation pressure and panel geometry of your specific design. Each production run on our three full lines includes in-process coating weight verification, giving you PVC inflatable tent fabric that maintains airtight integrity through repeated inflation and deflation cycles.
Pattern Printing and Custom Width for Production Efficiency
Inflatable tent fabricators cutting hundreds of identical panels need roll widths that minimize offcut waste. We supply PVC inflatable tent fabric roll stock in custom widths aligned to your nesting layout, reducing material loss at the cutting table [NEED_CITE: material utilization rates in coated fabric cutting operations]. Pattern printing is handled in-line, allowing branding, logos, or safety markings to be applied before the fabric reaches your fabrication floor. Sample rolls are developed within days so you can validate print registration and colour accuracy before committing to a full production order.
How GSM, Base Fabric, and Coating Interact in Inflatable Tent Fabric
Specifying inflatable structure fabric wholesale requires understanding three interdependent variables. The base fabric denier and weave density determine tensile and tear strength; the coating weight adds waterproofing and airtightness but also stiffness. A heavier GSM does not automatically mean a stronger fabric if the base cloth is loosely woven — the coating simply fills more gaps without adding structural integrity. Conversely, a tightly woven lightweight base with a thin, well-adhered coating can outperform a heavier alternative in tear resistance. For inflatable tents, the balance matters because panels must remain flexible enough to fold compactly yet rigid enough to hold shape under internal pressure. Our material specification sheet breaks down base fabric and coating separately so you can evaluate each contribution to the final GSM.
What Happens When Weld Parameters Ignore the Coating Composition
The most common fabrication failure in inflatable tent manufacturing is a welded seam that peels before the fabric itself reaches its load limit. This typically occurs when heat and pressure settings are calibrated for a generic PVC weight rather than the specific coating formulation on the roll [NEED_CITE: hot-air welding parameters for PVC coated fabrics per EN 13419]. A coating that is slightly harder or softer than expected will either under-fuse or burn through, creating a weak line that fails the first time the structure is pressurized. Because our PVC inflatable tent fabric rolls ship with a specification sheet stating exact coating composition, your fabrication team can set weld parameters from documented data rather than trial and error on the first few metres of each new batch.
Why Procurement Documentation Matters for Volume Roll Buyers
Every roll of PVC inflatable tent fabric we dispatch is backed by documentation tied to its specific production batch. This eliminates the guesswork that plagues container-load purchases where rolls arrive with no traceability to their coating run.
- Material specification sheet stating GSM, base fabric, and coating composition per roll batch
- Roll packing list with roll count, individual weight, and dimensional data for container loading verification
- Pre-shipment inspection record confirming colour uniformity and coating integrity across all rolls in the order
- UV-resistant treatment test documentation where applicable to the specified grade
- Certificate of origin and customs documentation prepared for international roll-stock shipment
Fabrication, Handling & Storage
- Set hot-air weld temperature based on the coating composition stated on the material specification sheet accompanying each roll
- Store rolls horizontally on racking to prevent permanent creasing in the PVC coating layer that affects panel flatness
- Allow rolls to acclimatize to workshop temperature before unrolling to avoid condensation between coating and base fabric
- Use pattern-printed rolls with the printed face inward during welding to protect branding from heat exposure at seam lines
- Plan cutting layout around the custom roll width to maximize panel yield and minimize offcut waste per roll
Specifying the Right Roll Stock for Your Inflatable Tent Line
To move forward with a quotation, share your target panel dimensions, annual roll consumption, and the inflation pressure your structures operate at. Let us know if you require pattern printing, a specific colour reference, or UV-resistant treatment for your market’s compliance standards. We will prepare sample rolls for your cutting and welding trials before any volume commitment.
Frequently Asked Questions
Q: How can I verify the stated GSM when the roll arrives at my factory?
A: Cut a measured sample from the roll end, weigh it on a calibrated scale, and compare against the GSM stated on the material specification sheet shipped with your order. We recommend checking at least one roll per batch. Our pre-shipment inspection record documents the GSM verification we performed before dispatch, giving you a baseline to compare against your incoming inspection results.
Q: How do you control colour consistency across multiple rolls in one order?
A: All rolls within a single purchase order are produced from the same pigment batch on the same coating line. Our QA team compares each finished roll against the approved colour reference under standardized lighting before winding. The pre-shipment inspection record confirms colour uniformity across the entire order, so you can cut panels from any roll without visible shade variation.
Q: What custom width options are available to improve my cutting efficiency?
A: We supply PVC inflatable tent fabric roll stock in widths matched to your panel nesting layout. Share your cutting plan with our R&D team and we will recommend a roll width that minimizes offcut waste. Custom widths are produced on our dedicated coating lines, and sample rolls in the target width are available for your trial before volume production begins.
Q: What welding parameters work best for this PVC coated fabric?
A: The material specification sheet accompanying each roll states the coating composition and weight, which your fabrication team should use to set hot-air or wedge weld temperature and speed. We recommend running weld tests on the first metre of each new batch to confirm peel strength before full production. Our technical team is available to advise on parameter adjustments if your initial tests show under-fusion or coating burn-through.
Q: How are rolls packed and protected for international container shipping?
A: Each roll is wrapped to protect the PVC coating surface from abrasion and moisture during transit. The roll packing list shipped with your order details roll count, individual weight, and dimensions so your logistics team can verify container loading against the manifest. We prepare certificate of origin and customs documentation to support smooth clearance at your destination port.