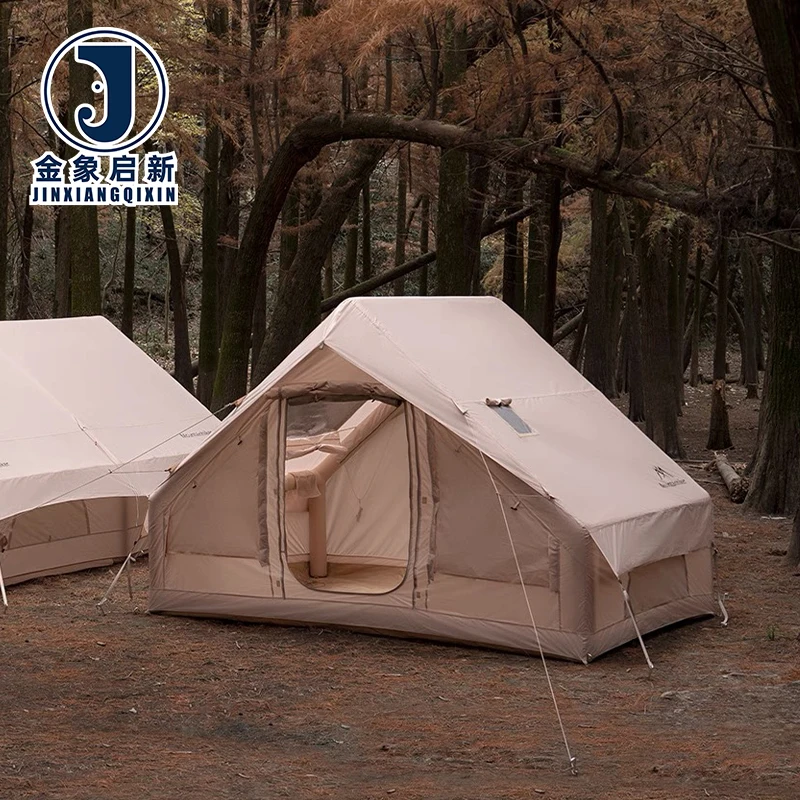
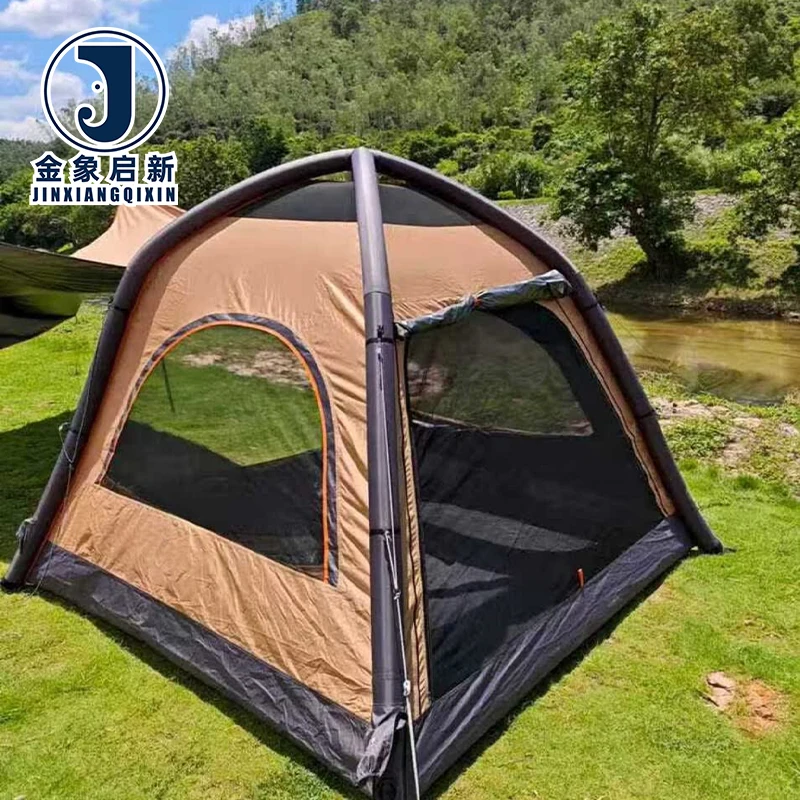
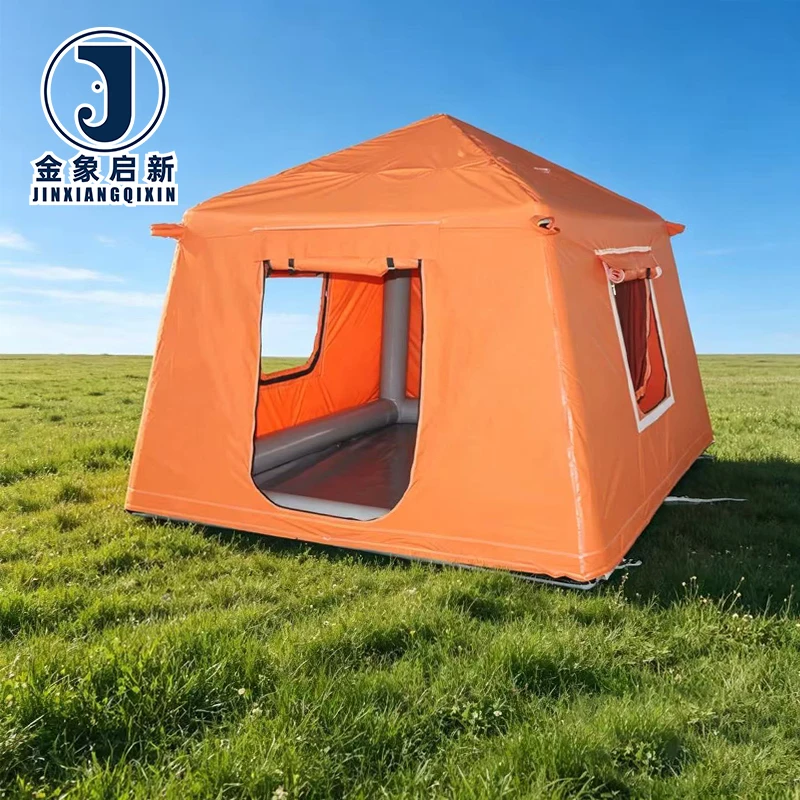
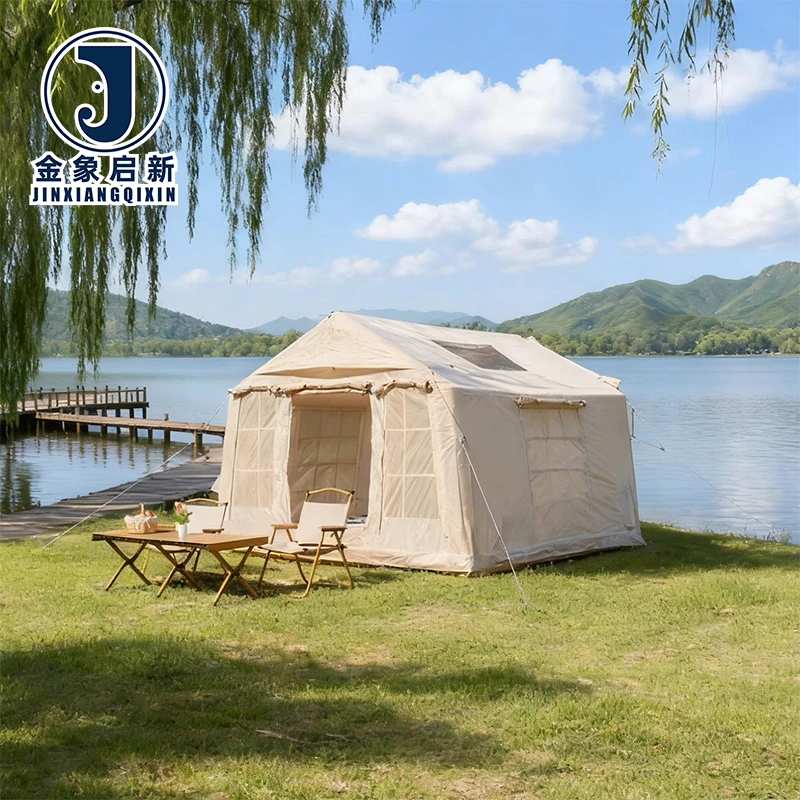
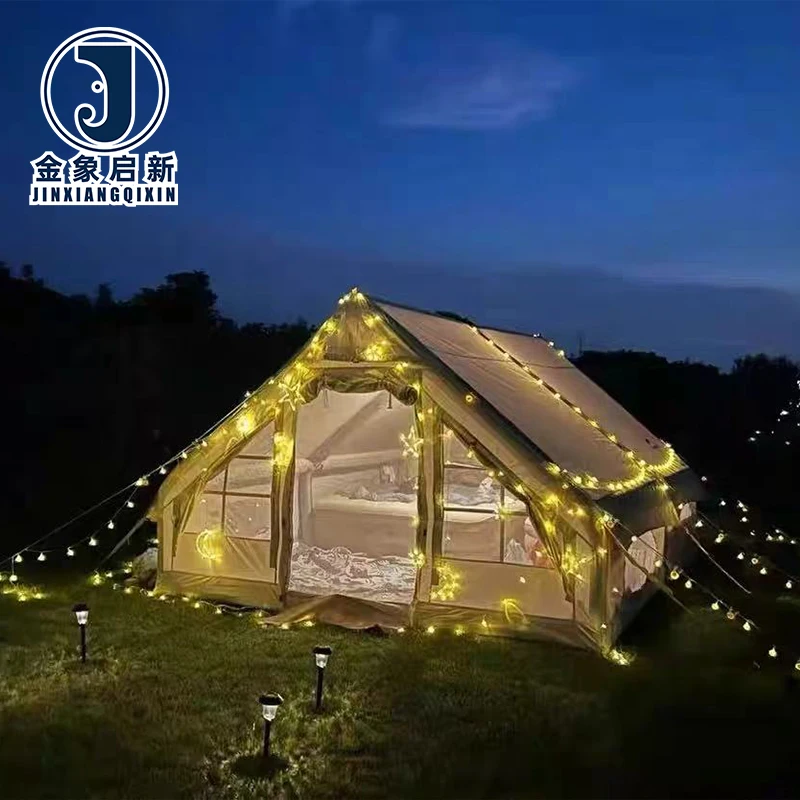
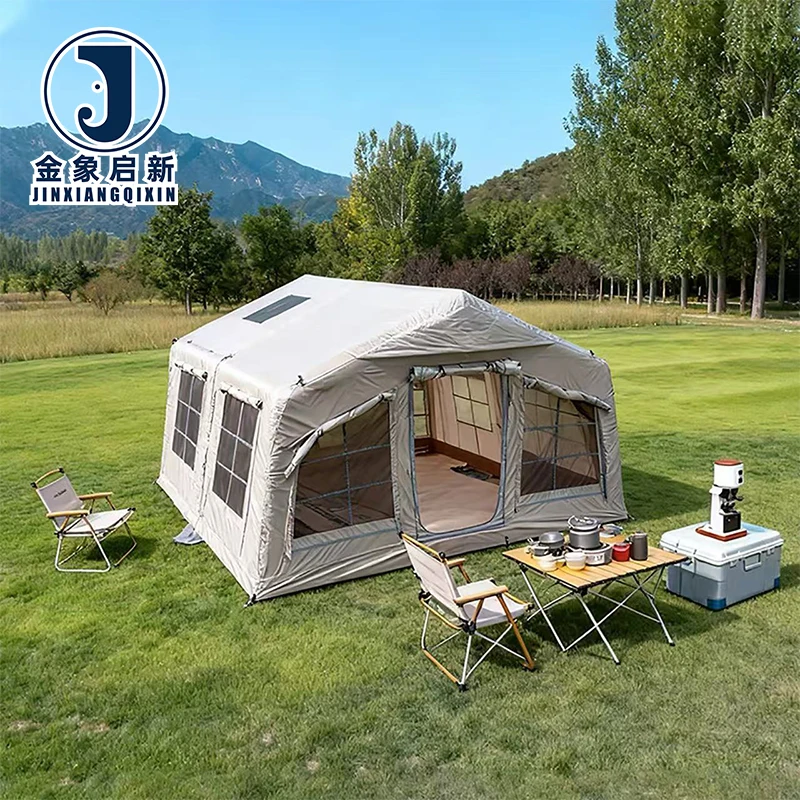
Description
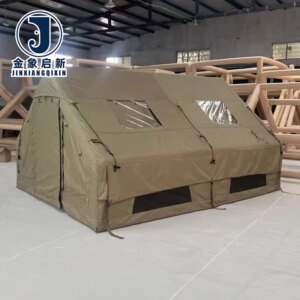
Roll-to-Roll Consistency — every PVC Inflatable Camping Tent fabric batch runs through dedicated QA checkpoints from coating to packing, eliminating the shade variation that forces rework on the cutting table.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Inflatable Tent |
| Core Material | PVC Tarpaulin (PVC knife-coated fabric) |
| Waterproof Rating | Tested to ASTM D751 |
| Tear Strength | Tested to ISO 13937-2 |
| UV Resistance | Tested to ISO 4892-2 |
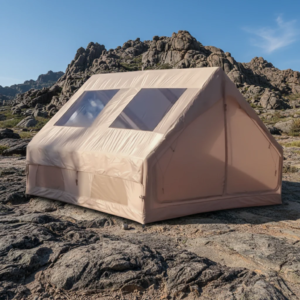
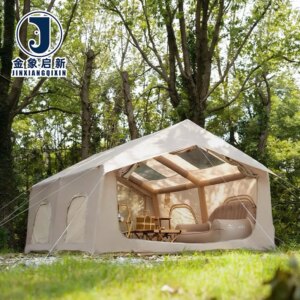
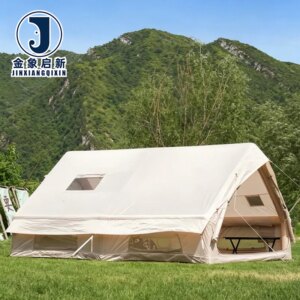
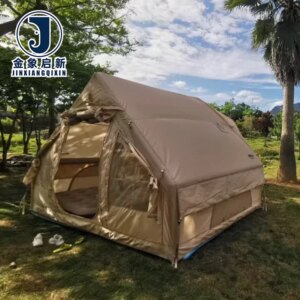
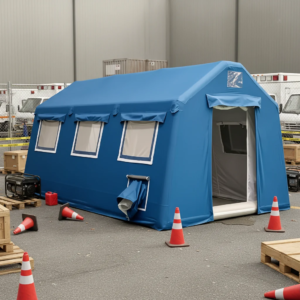
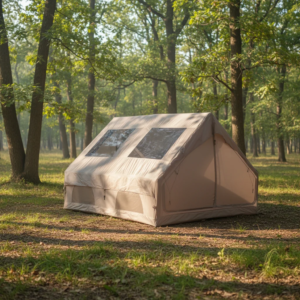
| Capacity | 4-6 Person |
| Construction | Single Layer |
| Opening Mechanism | Quick Automatic Opening |
| Customization | OEM & ODM (Material selection, Product design) |
| Certifications | ISO9001, ISO14001, ISO45001, CE |
| Production Lines | 3 full production lines |
| Processing Equipment | 36 sets of professional equipment |
Application Suitability
| Application | Exposure & Requirement |
|---|---|
| Temporary site offices for construction projects | Continuous UV and rain exposure, frequent relocation, puncture risk from site debris |
| Mobile equipment shelters for outdoor events | Rapid inflation cycles, crowd contact, abrasion from repeated setup and teardown |
| Auxiliary storage facilities for logistics operations | Sustained internal pressure, wind loading, moisture ingress prevention for stored goods |
| Commercial summer outdoor operations | High solar radiation, thermal expansion of air beams, seasonal storage between deployments |
Why Batch Consistency Matters More Than the Stated GSM on Inflatable Tent Fabric Roll Orders
A roll that matches the quotation on paper but drifts on the cutting table costs more than the fabric itself.
When manufacturers of inflatable structures buy PVC inflatable tent fabric by the roll, the assumption is that every roll in the container behaves identically under the heat welder and holds the same colour under daylight. In practice, coating weight can drift between production runs, and pigment dispersion can shift enough that two rolls installed side by side show a visible shade line. For a commercial tent fabricator running seasonal production, that inconsistency means wasted material, delayed shipments, and rejected panels. [NEED_CITE: coated fabric batch variation and its impact on welded seam integrity]
How Three Production Lines Maintain Uniform Coating Across Roll Stock
Maintaining colour and thickness uniformity across a large inflatable fabric wholesale order requires more than a single coating head. The three full production lines allow parallel runs where each line is dedicated to a specific width or colourway, reducing changeover contamination. The 36 sets of professional equipment include calendering and knife-coating stations that hold the PVC paste viscosity within a narrow band, which is the primary variable controlling final GSM. When viscosity drifts, the coating lays down heavier on one edge of the web, creating a roll that welds unevenly on the fabrication floor.
Colour Matching From Lab Dip to Container Load
The 10-person R&D team handles pigment formulation at the lab-dip stage before any production roll is cast. Once the buyer approves the reference swatch, that formulation is locked to the batch order number. During production, inline spectrophotometer checks compare the running web against the approved standard. Rolls that fall outside the tolerance window are diverted before they reach the packing stage, so the inflatable fabric wholesale shipment arrives with shade continuity from the first roll to the last. [NEED_CITE: spectrophotometric colour control in PVC coated fabric production]
What the Test Standards Actually Measure for Inflatable Structures
The waterproof rating tested to ASTM D751 confirms that the coated fabric resists hydrostatic penetration under the pressure conditions relevant to inflatable beam walls, where internal air pressure pushes the membrane outward and rain loads press inward simultaneously. Tear strength verified to ISO 13937-2 indicates how a small puncture or cut will propagate once the structure is inflated and under tension — a critical factor because inflatable tents rely on continuous air pressure, and a running tear can collapse an entire beam. UV resistance tested to ISO 4892-2 gives a baseline for how the PVC compound and pigment package hold up under accelerated weathering, which correlates to colour retention and flexibility loss during commercial summer deployments.
The Hidden Cost of Overlooking Roll-to-Roll Weld Behaviour
A fabric that looks correct on the specification sheet can still fail at the weld line if the coating formulation varies between rolls. PVC knife-coated fabric relies on the plasticiser content in the coating layer to fuse under hot-air or wedge welding. When one roll carries a slightly different plasticiser ratio, the weld temperature that works on roll A will under-fuse or burn through roll B. Fabricators who do not test weld parameters per roll end up with seams that peel under inflation pressure, often after the tent is deployed on site. [NEED_CITE: hot-air welding parameters and plasticiser migration in PVC coated textiles]
What This Supply Chain Delivers to Inflatable Tent Fabricators
Deep process control over coating weight and adhesion means the PVC tarpaulin core arrives with the peel strength needed for reliable heat-welded seams on inflatable beam construction. Three full production lines and 36 sets of equipment support bulk roll orders with on-time delivery, reducing the need for fabricators to carry excess safety stock. The 10-person R&D team develops custom width, colour, and printing specifications within days, shortening the sample-to-production cycle for seasonal tent launches. Dedicated QA and QC staff inspect every roll before packing, catching GSM drift and surface defects that would otherwise surface on the fabrication floor. ISO9001, ISO14001, ISO45001, and CE certifications provide the compliance documentation that cross-border buyers need for customs clearance and project tender submissions.
Documentation & Verification
- Material specification sheet listing GSM, base fabric denier, and PVC coating method per roll
- Batch inspection report covering ASTM D751 waterproof, ISO 13937-2 tear, and ISO 4892-2 UV results
- Roll packing list with container loading plan calculated by roll count and weight
- Certificate of origin and customs documentation package for cross-border procurement
- Pre-shipment inspection record traceable by purchase order and batch reference number
Fabrication, Handling & Storage
- Calibrate hot-air welder temperature per roll batch to account for PVC knife-coated fabric plasticiser variation
- Store rolls horizontally on racking to prevent edge compression marks on the single-layer membrane
- Allow cold-stored rolls to acclimatise before unrolling to avoid creasing the PVC coating surface
- Use compatible PVC solvent cement for field repairs on punctured inflatable beam sections
- Plan cutting layout to maximise yield from the supplied roll width and reduce offcuts
- Clean fabricated panels with mild detergent to preserve the UV-resistant coating surface
What to Include in Your Inquiry
Specify the target inflatable tent dimensions and expected deployment environment so the correct PVC tarpaulin grade can be recommended. State your required roll width, annual volume, and whether you need OEM or ODM support for product design. Confirm the fire-safety or regulatory standards applicable in your destination market so the right documentation package is prepared with your shipment.
Frequently Asked Questions
Q: How can I verify GSM consistency across rolls when the inflatable tent fabric shipment arrives?
A: Request the batch inspection report before dispatch, which records the measured coating weight per roll. On receipt, take spot samples from the first, middle, and last roll in the container and weigh them against the specification sheet. Any deviation beyond the stated tolerance should be reported immediately with photos and sample references for resolution.
Q: How is batch colour controlled so that every roll in an inflatable fabric wholesale order matches?
A: Pigment formulation is locked at the lab-dip approval stage and linked to your batch order number. During production, inline colour checks compare the running web against the approved swatch. Rolls that fall outside tolerance are removed before packing, ensuring shade continuity across the entire inflatable fabric wholesale shipment.
Q: What roll widths and container loading options are available for bulk inflatable tent fabric orders?
A: Roll width and length are configurable through the OEM and ODM service based on your cutting pattern and fabrication equipment. The packing list includes a container loading plan optimised by roll count and weight, and the logistics team provides loading diagrams to maximise container utilisation for your bulk order.
Q: Can I get custom colour matching or pattern printing, and what is the sample lead time?
A: The 10-person R&D team handles custom colour matching and pattern printing from lab dip to production sample. Once you submit your colour reference or artwork, a sample roll section is developed for approval. Confirm the required specifications and printing details at the inquiry stage to align the development timeline with your production schedule.
Q: What UV-resistant test documentation is included with each PVC inflatable tent fabric shipment?
A: Each shipment includes a batch inspection report referencing the ISO 4892-2 UV resistance test results for the specific production run. The material specification sheet also records the UV treatment formulation applied. Request these documents at the quotation stage to confirm they meet your market requirements before placing the order.