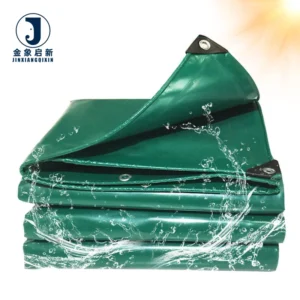
Description
Consistent roll-to-roll output — every production run of 450gsm PVC coated tarpaulin undergoes in-process QA with 100% pre-shipment inspection, securing uniform weight and colour across the entire bulk order.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | PVC Coated Tarpaulin |
| Weight | 450gsm |
| Base Fabric | High-tenacity polyester woven substrate |
| Coating Method | PVC double-sided coating |
| Finish | Double-Faced |
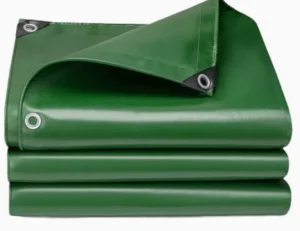
| Colour | Green (multiple colours available on request) |
| Water Resistance | Water resistant |
| UV Treatment | Anti-UV treated (test basis not stated in source — confirm requirement) |
| Flame Retardant | Flame retardant (grade not stated in source — confirm grade required for your market) |
| Key Features | Waterproof, anti-UV treated, flame retardant, double-faced coating |
Application Suitability
| Application | Exposure & Requirement |
|---|---|
| Tarpaulin distributor inventory | Bulk roll stock requiring batch-consistent colour and weight for regional resale |
| Construction site groundsheet | Ground moisture, soil abrasion, UV exposure, puncture from aggregate and tools |
| Equipment and machinery covers | Outdoor weathering, wind loading, UV degradation, repeated handling |
| Cargo and load protection | Rain ingress, road dust, wind flap, tie-down stress at contact points |
| Fabricator roll input | Welding compatibility, dimensional stability during cutting, colour matching across panels |
Why Stated GSM Does Not Guarantee Real-World Durability on Roll Stock
A 450gsm PVC coated tarpaulin roll is only as reliable as the coating adhesion and base fabric density behind the weight figure.
Buyers sourcing PVC coated tarpaulin roll wholesale often discover that the GSM printed on the quotation does not match the material that arrives on the container floor. Coating weight can drift across a single roll when line speed or knife gap varies mid-run, and the shortfall is invisible until the fabric tears prematurely on site. Without documented in-process weight checks tied to each roll, bulk buyers carry the entire risk of specification non-compliance. [NEED_CITE: tensile and tear test methods for coated fabrics per ISO 1421]
Roll-to-Roll Colour Uniformity Across Large Orders
Colour variation between rolls within the same order is a frequent complaint among tarpaulin importers restocking warehouse shelves. When two rolls of green PVC coated tarpaulin sit side by side on the racking, even a slight hue shift becomes visible and makes resale difficult. Batch consistency in pigment dosing and coating temperature is what separates a uniform shipment from a mixed batch. Confirming colour reference standards at the sample stage and verifying against the pre-shipment inspection record reduces the risk of visible mismatch once the rolls reach the distribution network.
Coating Adhesion and Its Effect on Fabrication
The double-faced PVC coating on this 450gsm material determines how well the fabric holds together at welded seams and cut edges. When coating adhesion is weak, the layers delaminate under flex stress — a problem that surfaces during fabrication rather than on the specification sheet. Fabricators cutting this roll stock into finished covers rely on consistent peel strength to produce welds that last as long as the base fabric. [NEED_CITE: peel strength and coating adhesion test methods for PVC coated fabrics]
How Base Fabric Density and Coating Weight Interact at 450gsm
The 450gsm weight grade results from the combined mass of the woven polyester base fabric and the PVC coating applied to both faces. Coating weight alone does not define tensile or tear performance; the denier of the yarns and the weave density in warp and weft directions determine how the fabric resists tearing under load. A lighter base fabric with a heavier coating may meet the GSM target but will underperform in tear resistance compared to a balanced construction. For roll stock buyers supplying fabricators, understanding this balance ensures the material holds up during cutting, welding, and end-use flexing. The double-faced coating contributes to uniform surface resistance on both sides, so neither face becomes a weak point when the fabric is folded or draped over irregular loads.
What Happens When Roll Consistency Is Not Verified Before Dispatch
When coating weight varies roll to roll, fabricators encounter inconsistent heat-seal behaviour — some rolls weld cleanly while others scorch or fail to bond at the same temperature setting. This forces production slowdowns and increases scrap rates. For tarpaulin distributors, inconsistent weight across rolls means some units sold to contractors will underperform in the field, generating warranty claims that erode margin. Colour drift between rolls also creates complaints when customers install panels cut from different rolls side by side. Pre-shipment inspection records that document per-roll weight and colour readings catch these deviations before the container is sealed. [NEED_CITE: coating weight variation impact on heat-seal performance in PVC fabrics]
Why Bulk Buyers Source This Roll Stock Here
Production control over coating weight and adhesion is maintained through in-process QA checks at each stage of the line, not just a final spot check. The facility runs three full production lines with 36 sets of professional equipment, giving the capacity to fulfil container-load orders within agreed lead times. A dedicated 10-person R&D team develops samples within days when a buyer needs a specific colour or width confirmed before committing to a bulk run. Every roll undergoes 100% inspection before shipment, with documented GSM readings and colour verification. Export documentation is prepared in-house, covering customs requirements for over 20 destination markets across North America, Europe, and Asia.
Documentation & Verification
- Material specification sheet confirming 450gsm, base fabric construction, and coating type for every roll order
- Pre-shipment inspection record showing per-roll weight verification and colour consistency data
- Roll packing list with individual roll dimensions, net weight, and container loading plan
- UV treatment and flame retardant test documentation supplied where applicable to your market requirements
- Certificate of origin and customs documentation prepared for destination country compliance
Fabrication, Handling & Storage
- Weld temperature and speed should be calibrated to the 450gsm double-faced coating for consistent seam strength
- Store rolls upright on end caps to prevent flat-spot deformation of the PVC coating surface
- Allow rolls to acclimatise to ambient temperature before unrolling to avoid coating crack in cold conditions
- Use sharp rotary blades when cutting to prevent fraying of the woven polyester base fabric edges
- Clean surfaces with mild detergent only — solvent-based cleaners may degrade the PVC coating finish
- Avoid stacking heavy items on stored rolls to preserve the coating surface and prevent permanent creasing
What to Include in Your Roll Stock Enquiry
Provide your target roll width and the standard lengths that fit your container loading plan. Specify the colour reference you need, and confirm whether you require sample rolls for weight and colour verification before authorising full production. Let us know your annual volume so we can align batch scheduling and maintain colour consistency across repeat orders. If your market requires documented flame retardant or anti-UV performance, state the grade or test standard so the correct formulation is applied.
Frequently Asked Questions
Q: How is 450gsm weight verified on each roll before shipment?
A: Every roll is weighed and measured during the pre-shipment inspection process. The recorded GSM is compared against the 450gsm specification, and any roll falling outside tolerance is held back. Buyers receive the inspection record with individual roll data alongside the packing list so they can verify compliance on arrival.
Q: What roll widths and lengths fit a standard 20ft or 40ft container?
A: Roll width and length are produced to match your container loading plan. Standard container configurations accommodate a range of widths and roll lengths. Providing your preferred dimensions at the enquiry stage allows us to calculate the optimal roll count and weight per container for efficient shipping.
Q: How is colour consistency maintained across multiple roll orders?
A: Colour reference is locked at the sample approval stage and used as the benchmark for every subsequent production run. In-process checks monitor pigment consistency during coating. The pre-shipment inspection includes a colour comparison against the approved reference to confirm batch-to-batch uniformity.
Q: What is the minimum order quantity for custom width or colour?
A: Minimum quantities depend on the specific width and colour requested. Custom runs require a production setup that influences the minimum threshold. Requesting a sample first allows you to confirm the material meets your requirements before the bulk order quantity is finalised and production begins.
Q: Can samples be provided for weight and colour confirmation before bulk production?
A: Yes, samples are developed within days for custom requirements. Buyers use these samples to verify the 450gsm weight, green colour, and double-faced coating before authorising full production. Sample approval forms part of the documented sales process and ensures alignment before the production run starts.