Description
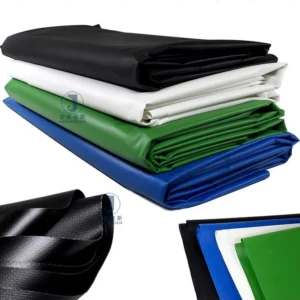
Roll-to-Roll Weight Verification — Every 550gsm roll leaving our facility is weighed and measured to confirm coating adhesion and GSM compliance before it reaches your warehouse.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | PVC Coated Tarpaulin Roll |
| Weight (GSM) | 550gsm |
| Total Thickness | 0.45mm |
| Base Fabric Denier Options | 200D×300D, 500D×500D, 840D×840D, 1000D×1000D |
| Color | Black |
| Surface Finish | Glossy or matte |
| Coating Material | PVC |
| Waterproof | Yes, fully coated construction |
| Temperature Range | -15°C to 70°C |
| UV Treatment | Available (grade to be specified per market requirement) |
| Flame Retardant | Available in treated grades (confirm required standard) |
| Anti-Fungal | Treated (specific standard to be confirmed) |
Application Suitability
| Application | Exposure & Requirement |
|---|---|
| Fish farming pond liners | Permanent water submersion, soil chemistry contact, puncture risk from substrate |
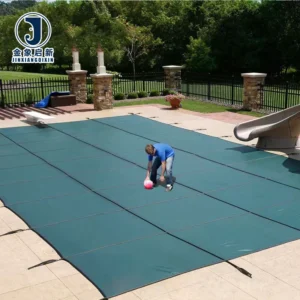
| Reservoir and water containment covers | Continuous moisture exposure, UV degradation potential, wind uplift stress |
| Agricultural stock covers | Outdoor weathering, mechanical handling abrasion, seasonal temperature fluctuation |
| Wholesale distributor stock | Batch-consistent colour and weight, predictable cutting yield, container loading efficiency |
Why Stated GSM Is Not Enough When Buying PVC Coated Tarpaulin Roll by the Container
A quoted GSM only matters if it survives the journey from the production line to your receiving dock.
The most common complaint among wholesale buyers is material arriving lighter than agreed. This happens when coating weight is not controlled at every stage of the lamination process. A 550gsm PVC coated tarpaulin roll that measures true on the first sample can drift lower across a production run if the coating head pressure or line speed varies. [NEED_CITE: coating weight control methods for PVC tarpaulin per ISO 3374]
Roll-to-Roll GSM Consistency Across a Bulk Shipment
Maintaining 550gsm across every roll in a multi-container order requires process discipline at the coating stage. The base fabric passes through the PVC coating head under controlled tension and temperature, and the coating weight is determined by knife gap, resin viscosity and line speed. Any drift in these variables shifts the GSM. Our three full production lines allow us to dedicate a single line to one specification for the entire production run, eliminating the cross-contamination that occurs when lines switch between grades mid-order. When you order PVC coated tarpaulin roll wholesale at 550gsm, the weight you receive on roll number fifty matches roll number one.
Colour and Surface Finish Matching Across the Batch
Black PVC coated fabric appears uniform under factory lighting but can show visible variation once multiple rolls are unrolled and laid side by side in daylight. Glossy and matte finishes behave differently under tension and during heat welding, which affects fabrication yield for converters cutting pond liners or water containment panels. [NEED_CITE: colour consistency measurement methods for coated textiles] Batch-to-batch colour matching is verified against a master swatch before the roll is released for packing, and surface finish is confirmed by both visual inspection and tactile check to ensure downstream welding parameters remain stable.
How Base Fabric Denier and Coating Weight Define Real-World Performance
The 0.45mm total thickness of this 550gsm grade is the result of the base fabric denier combined with the PVC coating weight applied to each face. A 500D×500D base provides a balanced tensile-to-weight ratio suitable for pond liners that need puncture resistance without excessive stiffness. Moving to an 840D×840D or 1000D×1000D denier increases tear propagation resistance, which matters when the liner is installed over uneven ground where point loads concentrate stress. The glossy finish sheds debris and simplifies cleaning, while the matte finish offers better ink adhesion for printed identification marks and reduces glare during installation in direct sunlight.
The Hidden Cost of Ignoring Weld Seam Performance
A pond liner fails most often not in the field of the fabric but at the weld seam where two panels overlap. If the PVC coating formulation or surface finish is inconsistent between rolls, the hot-wedge or high-frequency weld will bond unevenly, creating a weak line that separates under hydrostatic pressure. This failure mode is invisible at the time of fabrication and only appears once the pond is filled and the water load flexes the seam repeatedly. [NEED_CITE: weld seam strength testing methods for PVC coated fabrics] Specifying a consistent surface finish across all rolls in the same order is not a cosmetic concern — it is a structural requirement for any liner that relies on welded panel joins.
Why Source This PVC Coated Tarpaulin Roll From Jinan Jinxiang
Nearly 30 years of continuous coated fabric production gives us process data across thousands of production runs, allowing us to predict how a specific denier and coating weight combination will behave during welding and long-term water exposure. Three full production lines and 36 sets of professional equipment mean that a bulk order of 550gsm black roll stock can be completed on a dedicated line without the scheduling delays that affect smaller manufacturers. The 10-person R&D team develops sample swatches in standard and custom widths within days, letting you test weld parameters and cutting yield before committing to a full container. Dedicated QA/QC personnel inspect every roll at each production stage, and a 100% pre-shipment inspection verifies GSM, colour, and surface finish against the original specification before any roll is packed for dispatch.
Documentation & Verification
- Material specification sheet confirming 550gsm, denier, and coating weight per roll batch
- Pre-shipment inspection record with roll-by-roll weight and visual check before dispatch
- Roll packing list detailing roll count, net weight, and dimensions for container loading plans
- Certificate of origin and customs documentation supporting export clearance
- UV and flame-retardant test reports supplied when treated grades are specified
Fabrication, Handling & Storage
- Hot-wedge weld temperature should be adjusted for 0.45mm total thickness and tested on off-cuts first
- Store black PVC rolls vertically on pallets to prevent flat-spot creasing on the coating surface
- Unroll at ambient temperature above 5°C to avoid coating stiffness and cracking at the fold line
- Cut pond liner panels with allowance for thermal expansion in the 550gsm PVC membrane under sun exposure
- Use compatible PVC solvent adhesive for field repairs on 550gsm material, matching the surface finish
What to Specify When Requesting a Quotation
To move from inquiry to sample, provide the end-use environment so we can recommend the appropriate denier from the available range. Confirm whether you need glossy or matte finish based on your welding equipment and whether UV or flame-retardant treatment is required for your market. State the roll widths and lengths that optimise your cutting pattern, and indicate your annual volume so we can plan production line allocation accordingly.
Frequently Asked Questions
Q: How is 550gsm verified before shipment and what should I check on arrival?
A: Every roll is weighed and measured during our 100% pre-shipment inspection, and the results are recorded on the inspection report that ships with the container. On arrival, we recommend cutting a known-area sample from each roll and weighing it on a calibrated scale to confirm the GSM matches the documentation.
Q: What roll widths and lengths are available, and how do I optimise for my cutting pattern?
A: Standard widths and lengths are stocked for immediate loading. For custom widths that reduce off-cut waste in your pond liner fabrication, provide your panel dimensions and we will calculate the optimal roll width and length to maximise yield per square metre.
Q: How do you ensure colour consistency across multiple black rolls in the same order?
A: All rolls in a single production run are coated from the same PVC batch and verified against a master black swatch before packing. A pre-shipment sample from the production run is available on request so you can confirm the colour and finish match your warehouse stock.
Q: How are rolls packed and loaded to prevent creasing or coating damage in transit?
A: Rolls are packed in carton or bale wrapping and loaded vertically or horizontally depending on container configuration. The roll packing list details the loading plan, and we recommend reviewing the packing method against your unloading equipment to prevent coating scuff during handling.
Q: What welding temperature and technique suit 550gsm 0.45mm PVC coated fabric?
A: Hot-wedge and high-frequency welding both work on this grade. The 0.45mm thickness requires a specific temperature and dwell time that should be tested on sample off-cuts first. Request a fabrication sample and we will include welding guidance matched to the surface finish you specify.